Blogs
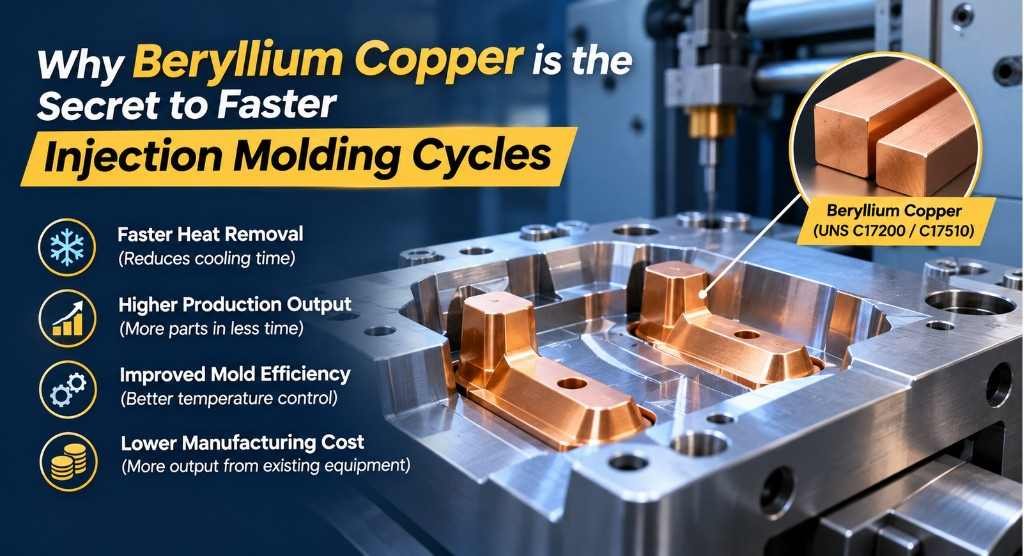
Why Beryllium Copper Is the Secret to Faster Injection Molding Cycles: 9 Powerful Benefits of UNS C17200 & C17510
Beryllium Copper Injection Molding helps manufacturers reduce cooling time, improve mold performance, and increase production efficiency while maintaining high-quality plastic components.
In injection molding, every second matters. When cooling takes longer, production slows, energy consumption increases, and manufacturing costs rise.
What if faster production depends on better mold materials rather than expensive new machines?
This is where Beryllium Copper Injection Molding offers a powerful advantage.
Unlike conventional mold steels, beryllium copper alloys provide higher thermal conductivity, helping critical mold components dissipate heat efficiently while maintaining mechanical strength and durability.
At DOMADIA™, we understand how the right specialty alloy can improve productivity, mold longevity, and cost efficiency.
In this guide, we explore 9 powerful benefits of Beryllium Copper Injection Molding, covering chemical composition, thermal properties, technical specifications, industrial applications, international standards, available forms, and material selection.
1. What Is Beryllium Copper, and Why Is It Used in Injection Molding?
Beryllium copper, commonly abbreviated as BeCu, is a copper-based alloy containing a controlled percentage of beryllium and, depending on the grade, other alloying elements.
It is valued for its combination of:
- High thermal conductivity compared with conventional tool steels
- Good mechanical strength
- Hardness and wear resistance
- Corrosion resistance
- Good dimensional stability when properly processed
- Excellent electrical conductivity in selected grades
- Suitability for precision-machined industrial components
These properties make beryllium copper useful in injection molding applications where rapid heat transfer and adequate mechanical performance are both important.
Understanding the two important UNS grades
UNS C17200 — High-Strength Beryllium Copper
Primarily selected when high strength, hardness, and wear resistance are essential alongside improved heat transfer compared with mold steel.
UNS C17510 — High-Conductivity Beryllium Copper
Particularly attractive for selected mold inserts and thermal-management components where higher conductivity is valuable and the design permits its mechanical properties.
Although both alloys belong to the copper-beryllium family, they are not interchangeable in every application.
The correct selection depends on mold temperature, injection pressure, component geometry, cooling requirements, surface finish, and expected service life.
2. Why Cooling Time Is the Hidden Cost of Injection Molding
Injection molding cycle time is generally divided into several stages:
- Mold closing and clamping
- Injection and filling
- Packing and holding
- Cooling and solidification
- Mold opening and component ejection
Cooling frequently represents a major portion of the cycle, although the actual percentage varies with the polymer, wall thickness, geometry, and process.
If a molded component cannot be safely ejected until its temperature falls sufficiently, the machine must wait.
That waiting time affects:
- Production output
- Machine utilization
- Energy consumption per acceptable component
- Manufacturing lead time
- Production scheduling
- Overall cost per component
This is why mold thermal management is so important.
A material that transfers heat more efficiently from a hot region to the cooling system may reduce localized cooling limitations.
Beryllium copper can help improve this heat-transfer pathway when it is correctly integrated into the mold design.
3. Nine Powerful Benefits of Beryllium Copper in Injection Molding

Benefit 1: Higher Thermal Conductivity Can Reduce Cooling Time
One of the biggest advantages of Beryllium Copper Injection Molding is faster heat transfer.
Beryllium copper conducts heat much better than conventional mold steels. This helps plastic components cool more efficiently and may reduce the time required to complete each molding cycle.
Thermal Conductivity Comparison
| Material | Thermal Conductivity |
| UNS C17200 | 105–130 W/m·K |
| UNS C17510 | 190–240 W/m·K |
| P20 Mold Steel | 28–35 W/m·K |
| H13 Tool Steel | 24–30 W/m·K |
Note: These are approximate values. Actual conductivity depends on the material grade and condition.
UNS C17510 offers significantly higher thermal conductivity than conventional mold steels, making it useful for mold inserts that require efficient cooling.
For example, if a plastic component takes too long to cool, using a suitable beryllium copper insert may help remove heat faster.
This can provide several benefits:
- Reduced cooling time
- Faster injection molding cycles
- Increased production efficiency
- Better temperature control
- Potentially lower manufacturing costs
However, actual cooling improvements depend on mold design, plastic material, and cooling-system performance.
In simple terms, better heat transfer can mean faster production and improved mold efficiency.
Benefit 2: Improved Cooling Uniformity Can Reduce Warpage
One of the most frustrating problems in injection molding is producing a component that looks correct inside the mold but changes shape after ejection.
Uneven cooling can cause different regions of a plastic component to shrink at different rates.
This may contribute to:
- Warpage
- Dimensional variation
- Internal stress
- Uneven shrinkage
- Assembly difficulties
- Increased rejection rates
A strategically placed beryllium copper insert may help reduce temperature differences in critical mold regions.
For example, a thick plastic boss may retain heat longer than the surrounding thin-wall sections.
Replacing a suitable steel core or insert with a higher-conductivity copper alloy can improve heat extraction from that localized region.
The result may be more consistent cooling and better dimensional repeatability, provided the entire molding process is properly controlled.
Benefit 3: Better Heat Removal from Deep Cores and Difficult Geometries
Complex plastic components often contain deep cavities, ribs, narrow cores, and thick intersections.
These geometries can create localized hot spots because conventional cooling channels cannot always be positioned close to the required surfaces.
Beryllium copper inserts may provide an alternative heat-transfer path in such areas.
Common examples include:
- Deep core pins
- Narrow mold cores
- Thread-forming components
- Thick-section inserts
- Difficult-to-cool cavity regions
- Localized hot spots near ribs and bosses
In these applications, the material acts as a thermal-management component rather than simply a structural mold material.
This distinction is important because the greatest benefit may come from replacing only a small, carefully selected section of the mold.
Benefit 4: Increase Production Without Buying a New Machine
Buying a new injection molding machine can be expensive. However, manufacturers may be able to increase production by improving the cooling efficiency of their existing molds.
Beryllium Copper Injection Molding can help reduce cooling time by transferring heat away from critical mold areas more efficiently.
For example, consider a factory operating for 20 hours daily:
- Before improvement: 40 seconds per cycle = 1,800 components per day.
- After improvement: 34 seconds per cycle = approximately 2,118 components per day.
- Additional production: Approximately 318 components daily.
This example shows a potential 17.6% increase in production output without purchasing another machine.
Actual improvements depend on mold design, plastic material, and cooling conditions.
By using suitable beryllium copper inserts, manufacturers may improve productivity, reduce manufacturing costs, and make better use of existing equipment.
Benefit 5: Improved Temperature Control Can Support Better Surface Quality
Surface appearance is critical in consumer electronics, automotive interiors, medical-device housings, and precision plastic products.
Uneven mold temperatures may contribute to visible defects, including:
- Gloss variation
- Sink marks
- Surface inconsistencies
- Localized shrinkage
- Certain dimensional defects
High-conductivity inserts can help manage localized temperature differences when properly designed.
For example, a mold region containing a thick plastic feature may require additional heat extraction to achieve acceptable appearance and dimensional stability.
Beryllium copper may help address this problem without redesigning the entire mold.
However, not every surface defect is caused by cooling. Material drying, injection speed, packing pressure, gate design, and mold temperature must also be investigated.
Benefit 6: High Strength Makes Selected Grades Suitable for Demanding Mold Components
Pure copper offers excellent thermal conductivity but relatively low mechanical strength. Beryllium Copper Injection Molding provides a better balance of heat transfer, strength, and durability for demanding mold components.
Injection molds experience repeated pressure, thermal cycling, and mechanical stress. Therefore, Beryllium Copper Injection Molding benefits from alloys that can withstand these conditions while improving cooling efficiency.
UNS C17200 offers high strength and hardness through precipitation hardening, making it suitable for mechanically demanding applications.
Meanwhile, UNS C17510 provides higher thermal conductivity but lower maximum strength than C17200.
For successful Beryllium Copper Injection Molding, engineers must balance thermal performance, mechanical strength, and long-term mold reliability.
Benefit 7: Corrosion Resistance Can Support Mold Reliability
Injection molds face moisture, condensation, cleaning chemicals, and potentially corrosive processing conditions. Beryllium Copper Injection Molding offers useful corrosion resistance, supporting reliable mold performance and durability.
However, Beryllium Copper Injection Molding components are not resistant to every chemical environment. Certain polymers, additives, and degradation products, particularly those generated during improper PVC processing, can cause corrosion.
Therefore, successful Beryllium Copper Injection Molding requires careful material selection and chemical compatibility evaluation to ensure long-term mold reliability.
Benefit 8: Targeted Inserts Can Improve the Economics of Mold Design
A complete injection mold manufactured from beryllium copper would often be unnecessarily expensive and may not provide the best overall mechanical performance.
A more practical approach is frequently to use conventional tool steel for the main mold structure and install beryllium copper only in thermally demanding locations.
This hybrid design approach can provide several advantages:
- Lower specialty-alloy consumption
- Improved heat extraction in selected areas
- Retention of steel strength in the main mold structure
- Easier replacement of individual inserts
- Potentially lower total tooling investment than an all-copper-alloy design
The objective is not to replace every steel component.
It is to position the right alloy where it delivers the greatest engineering value.
Benefit 9: Longer-Term Productivity Can Justify a Higher Material Price
Beryllium Copper Injection Molding may involve higher initial material costs than conventional mold steels, but its potential long-term benefits can make the investment worthwhile.
By improving heat transfer and reducing cooling delays, Beryllium Copper Injection Molding can help manufacturers increase productivity, reduce rejection rates, and optimize machine utilization.
For high-volume production, even small cycle-time savings may offset the additional tooling investment. However, low-volume applications require careful cost evaluation.
The real value lies in performance, not just purchase price.
At DOMADIA™, we encourage manufacturers to evaluate Beryllium Copper Injection Molding through total cost of ownership, considering tooling costs, maintenance, production efficiency, and long-term savings.
4. Chemical Composition of Beryllium Copper Mold Alloys
Chemical composition directly influences strength, conductivity, heat-treatment response, and industrial suitability.
The following are representative composition limits for two important copper-beryllium grades.
| Element | UNS C17200 | UNS C17510 |
| Copper | Balance | Balance |
| Beryllium | 1.80–2.00% | 0.20–0.60% |
| Nickel | Part of specified minor-element limits | 1.40–2.20% |
| Cobalt | Part of specified minor-element limits | — |
| Other elements | Controlled by applicable specification | Controlled by applicable specification |
Weight percentages, indicative of common alloy specifications. C17200 has combined minor-element requirements; refer to the applicable ASTM standard and mill certificate for exact limits.
Why does composition matter?
UNS C17200 contains relatively more beryllium, supporting a strong precipitation-hardening response.
UNS C17510 contains less beryllium and uses nickel as an important alloying element.
Its composition supports a different balance between conductivity and mechanical strength.
For injection molding, these differences affect how the material performs under thermal and mechanical loading.
5. Technical Specifications and Mechanical Properties
| Property | UNS C17200 | UNS C17510 |
| Alloy family | High-strength copper-beryllium | High-conductivity copper-nickel-beryllium |
| Density | Approx. 8.25 g/cm³ | Approx. 8.8 g/cm³ |
| Thermal conductivity | 105–130 W/m·K | 190–240 W/m·K |
| Electrical conductivity | Approx. 18–25% IACS | Approx. 45–60% IACS |
| Ultimate tensile strength | Approx. 1,100–1,400 MPa | Approx. 600–900 MPa |
| Hardness | Approx. 36–42 HRC | Approx. 20–30 HRC |
| Main advantage | Higher strength and hardness | Higher thermal conductivity |
Representative values for selected processed or hardened conditions, not simultaneous guaranteed minimums. Product form, heat treatment, and supplier data may substantially change the values.
A critical engineering point is that thermal conductivity and maximum hardness do not necessarily occur in the same material condition.
Therefore, procurement teams should not select a mold insert based on UNS designation alone.
They should also confirm the material temper, processing condition, dimensions, and certified properties.
6. Beryllium Copper vs Conventional Mold Steel
The choice between beryllium copper and tool steel is not a competition where one material wins every category.
Each material serves different engineering priorities.
| Selection factor | Beryllium copper | Conventional mold steel |
| Heat transfer | Generally much higher | Lower |
| High-load structural applications | Grade and design dependent | Often preferred |
| Wear resistance | Good in suitable grades | Often excellent with suitable treatment |
| Material cost | Higher | Generally lower |
| Localized hot-spot cooling | Particularly attractive | May require additional cooling design |
| Large structural mold components | Less commonly preferred | Widely used |
| Targeted thermal inserts | Strong application potential | Conventional option |
For high-volume plastic molding, the most effective solution may combine both materials.
Steel provides the main structural support, while a beryllium copper insert helps transfer heat from a critical region.
This approach can balance strength, cooling performance, and tooling economics.
7. Industrial Applications of Beryllium Copper in Injection Molding

Automotive Plastic Components
Beryllium Copper Injection Molding supports the production of connector housings, clips, complex ribs, and precision plastic components by improving cooling uniformity, dimensional accuracy, and production efficiency.
Electrical and Electronics Manufacturing
In electronics manufacturing, Beryllium Copper Injection Molding helps manage localized heat in intricate plastic connectors, insulating components, and small housings through specialized mold cores and inserts.
Medical Device Components
Beryllium Copper Injection Molding can support precision medical plastic manufacturing through controlled thermal conditions and consistent component quality, subject to process validation and contamination-control requirements.
Packaging and Consumer Products
For high-volume manufacturing of caps, closures, and consumer plastic products, Beryllium Copper Injection Molding can help reduce cooling delays and improve production efficiency.
Precision Mold Tooling
Beryllium Copper Injection Molding is valuable for selected core pins, mold inserts, cavity details, and difficult-to-cool features where efficient heat transfer and mechanical performance are essential.
8. International Standards for Beryllium Copper Alloys
International standards help establish material identity, composition, product-form requirements, and testing expectations.
Important standards include:
| Standard | Relevance |
| ASTM B194/B194M | Copper-beryllium alloy plate, sheet, strip, and rolled bar |
| ASTM B196/B196M | Copper-beryllium alloy rod and bar |
| ASTM B197/B197M | Copper-beryllium alloy wire |
| ASTM B441 | Copper-cobalt-beryllium, copper-nickel-beryllium, and related rod and bar products |
| ASTM E8/E8M | Tensile testing of metallic materials |
| ASTM E18 | Rockwell hardness testing |
Not every standard applies to every grade, shape, or supply condition.
For example, UNS C17510 rod and bar requirements should be checked against the applicable high-conductivity copper-alloy specification rather than automatically applying a C17200 standard.
What should manufacturers verify before purchasing?
A technical purchase specification should identify the UNS grade, applicable material standard, material condition, required dimensions, tolerances, mechanical-property requirements, and inspection documentation.
For demanding tooling, certified thermal-conductivity data may also be valuable.
9. Available Shapes and Forms of Beryllium Copper
Depending on the alloy grade and supplier availability, beryllium copper may be sourced in several forms.
| Material form | Typical application |
| Round bars and rods | Core pins, precision inserts, machined components |
| Flat bars | Insert blanks and tooling components |
| Plates | Mold inserts and thermal-management sections |
| Blocks | Custom-machined cavity and core inserts |
| Sheets and strips | Specialized fabricated components |
| Wires | Electrical and spring-related applications |
| Custom-machined parts | Application-specific tooling components |
Availability varies significantly by grade, size, condition, and manufacturing route.
At DOMADIA™, customers can discuss their requirements for specialty copper alloys, including required dimensions, material specifications, and intended applications.
10. When Should Engineers Choose UNS C17200 or UNS C17510?
Choosing the right beryllium copper grade depends on your mold’s strength and cooling requirements.
- UNS C17200: Best for high strength, hardness, and wear resistance.
- UNS C17510: Best for higher thermal conductivity and faster heat removal.
- Both Grades: Suitable for selected injection molding applications, depending on mold design.
In simple terms: Choose UNS C17200 for strength and UNS C17510 for better cooling efficiency.
DOMADIA™ helps manufacturers select suitable beryllium copper grades for their industrial requirements.
11. Can Beryllium Copper Reduce Manufacturing Costs?
Yes, in suitable applications, but the savings must be calculated rather than assumed.
Consider a mold insert that costs more initially but produces a measurable reduction in cycle time.
The potential financial benefits may include increased machine capacity, fewer rejected parts, reduced production delays, and lower processing cost per acceptable component.
A simple payback calculation is:
\[ \text{Payback period}=\frac{\text{Additional tooling investment}}{\text{Net savings per period}} \]
For example, if an upgraded insert requires an additional ₹80,000 and produces verified net savings of ₹20,000 per month, the simple payback period would be four months.
This is only an illustrative calculation. Actual savings depend on production demand, machine economics, quality yield, tool maintenance, and operating conditions.
A higher initial material price may therefore be justified when the total production benefit is sufficiently large.
12. Environmental Benefits of Improved Mold Efficiency
Sustainability in manufacturing depends on efficient energy use, reduced material waste, and longer equipment life. Beryllium Copper Injection Molding can support these goals by improving cooling efficiency and potentially reducing production cycle times.
With improved thermal management, Beryllium Copper Injection Molding may help reduce energy consumption per acceptable component, minimize scrap, and improve equipment utilization. Properly designed mold components may also provide longer service life, reducing replacement requirements and associated material waste.
However, the environmental benefits of Beryllium Copper Injection Molding must be evaluated against the impacts of alloy production and processing. Beryllium-containing materials require appropriate safety controls, especially during machining operations that generate airborne dust or fumes.
At DOMADIA™, we believe responsible Beryllium Copper Injection Molding involves selecting durable materials, improving manufacturing efficiency, and supporting sustainable industrial practices through measurable energy savings, reduced scrap, and optimized tooling performance.material selection should support both manufacturing efficiency and responsible industrial practices.
13. Important Safety Considerations When Machining Beryllium Copper
Beryllium copper is a valuable engineering alloy, but Beryllium Copper Injection Molding requires responsible material handling and workplace safety practices.
During machining, grinding, polishing, or certain thermal operations, airborne beryllium-containing dust and fumes can create serious health risks, including chronic beryllium disease.
For safe Beryllium Copper Injection Molding, manufacturers should use appropriate local exhaust ventilation, control airborne particles, follow safe machining and housekeeping procedures, and provide suitable personal protective equipment.
Additionally, Beryllium Copper Injection Molding operations should follow supplier safety data sheets and applicable occupational exposure regulations, while avoiding uncontrolled dry grinding and dust-generating activities.
Although finished solid components present different exposure conditions than airborne particles, Beryllium Copper Injection Molding still requires proper handling, processing controls, and employee safety awareness.al.
14. Why DOMADIA™ for Beryllium Copper Mold Materials?

Choosing the correct copper alloy is not simply about purchasing metal.
It requires understanding how material properties affect actual industrial performance.
At DOMADIA™, we focus on helping industrial buyers, engineers, tooling manufacturers, and procurement professionals evaluate specialty materials according to their technical requirements.
Material-focused sourcing
At DOMADIA™, we understand the importance of selecting the correct UNS grade, material condition, and dimensions for Beryllium Copper Injection Molding applications.
Support for specialized requirements
Beryllium Copper Injection Molding may require rods, bars, blocks, plates, or custom-sized blanks. DOMADIA™ supports customers in discussing suitable material specifications and sourcing options.
Understanding performance beyond price
Successful Beryllium Copper Injection Molding depends on balancing material cost, thermal performance, durability, and long-term manufacturing efficiency.
Industrial material expertise
DOMADIA™ specializes in advanced industrial materials and specialty alloys, supporting manufacturers seeking reliable Beryllium Copper Injection Molding solutions.
Whether your project requires high-strength copper alloys, high thermal conductivity, or precision engineering materials, DOMADIA™ helps you identify suitable specifications for improved performance and productivity.
Conclusion: Faster Injection Molding Starts with Smarter Material Selection
Beryllium Copper Injection Molding helps manufacturers improve heat transfer, eliminate localized hot spots, and reduce cooling delays without investing in new equipment.
With excellent thermal conductivity and mechanical performance, Beryllium Copper Injection Molding benefits from UNS C17200 for strength and hardness, while UNS C17510 offers higher thermal conductivity.
However, successful results depend on proper mold design, cooling efficiency, polymer characteristics, and material selection.
The secret to faster production is using the right alloy in the right location.
For manufacturers seeking shorter cycle times and improved productivity, Beryllium Copper Injection Molding solutions from DOMADIA™ can support efficient tooling and long-term performance.
Accelerate Injection Molding Performance with DOMADIA™ Beryllium Copper!
Reduce cooling bottlenecks, improve mold efficiency, and unlock greater production potential with high-performance Beryllium Copper UNS C17200 and UNS C17510.
Partner with DOMADIA™ for specialty copper alloy solutions tailored to your precision tooling and injection molding requirements.
Contact DOMADIA™ Today to discuss your material specifications and sourcing needs.
Talk to: Er.Pankaj Domadia | Kairav Domadia | Aadil Domadia | Pragati Sanap | Pooja N N
#BerylliumCopper #InjectionMolding #UNSC17200 #UNSC17510 #MoldCooling #PlasticManufacturing #MoldDesign #ThermalConductivity #PrecisionEngineering #IndustrialMaterials #DOMADIA
Directly whatsapp us for an Enquiry: https://wa.link/kairav
We’ve supplied to Mumbai, Pune, Indore, Jaipur, and Surat—serving industries across Maharashtra, Madhya Pradesh, Rajasthan, Gujarat, and Goa, with exports to Germany, USA, Japan, South Korea, and Italy.